Measure tag-band packing time before estimating savings
Define a fair timing comparison, include preparation and rework, and separate measured packing time from assumptions about labour savings.
Choose the task you want to compare
If you are considering a different tag-and-band arrangement, start with a specific question: how much time does your team spend preparing and applying it to a finished pack? Write down the current process and the proposed process before timing either one.
Include the steps that happen away from the packing bench. If tags and bands are prepared in advance, record that work as well as application time. Keep the comparison tied to the same finished product and presentation requirement so the result answers a purchasing question your business can use.
Set clear start and finish points
Choose an observable starting point, such as collecting the materials for a defined batch, and a finishing point, such as completing inspection of that batch. Decide which activities belong inside the measurement and use the same boundaries for both arrangements.
Record preparation, application and inspection separately where practical. Note replenishment, interruptions and rework rather than silently removing them from the total. If an interruption is unrelated to the packaging task, show the time and explain whether it is included. Keep the original observations alongside any adjusted result.
Keep the comparison representative
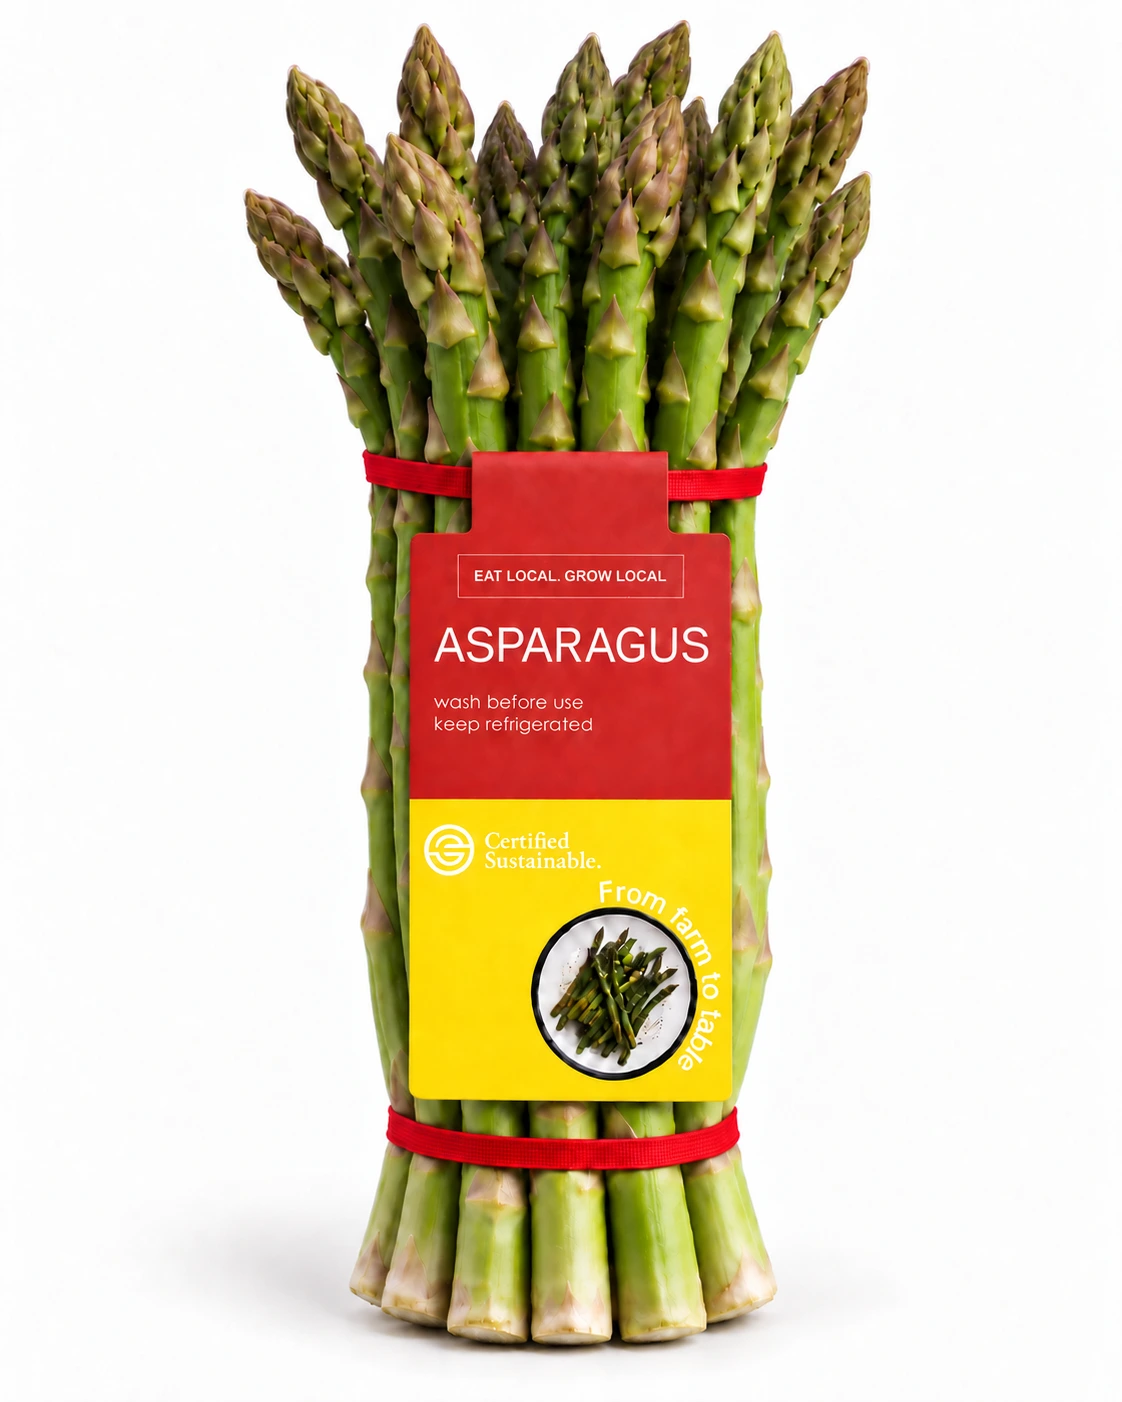
Use comparable products, bunch sizes or pack shapes and the same acceptance criteria. Record who completed the work, the batch size and the workstation arrangement. Give the operator a chance to understand an unfamiliar method before collecting the observations used for comparison.
Avoid choosing only the quickest run. Repeat the exercise across representative work and retain each result, including awkward packs and corrections. If conditions differ between runs, describe the differences. A short demonstration can guide the next assessment, but it should not become an unsupported claim about everyday production.
Calculate time per acceptable pack
Divide the recorded time by the number of finished packs that meet the agreed criteria. Include time spent correcting packs within the measurement boundary, and count each accepted finished pack once. Record rejected packs separately so the final figure has context.
For a hypothetical example, a batch taking 18 minutes to produce 120 acceptable packs averages 9 seconds per pack: 18 multiplied by 60, divided by 120. This is an arithmetic illustration, not an ANYTAPE result or a target. If no packs are acceptable, report the unsuccessful run rather than calculating a time per acceptable pack.
Keep the business conclusion separate
A measured time difference is one input to a purchasing decision. Before describing it as a labour saving, identify how the change would affect actual work allocation, staffing or paid hours. Keep any assumed production volume and labour rate visible, and label projected outcomes as estimates.
Compare the full proposal as well: packaging quantity and price basis, preparation work, equipment requirements, print or setup charges, and observed rejects. Confirm that the finished packs still meet your requirements after normal handling. Do not let a faster application result replace the separate assessment of fit, presentation and suitability.
Turn the observations into an enquiry
Prepare a brief record with the product or crop, tag and band references, photographs, batch sizes, timing boundaries and observations. Explain which task you want to simplify and which presentation requirements must remain. Ask the supplier to confirm the proposed specification and sample options.
Use the Tag Bands product link below when preparing your enquiry. Confirm availability and timing directly, then agree what a useful assessment would involve. Keep any later performance statement tied to the method, conditions and results your team actually recorded.